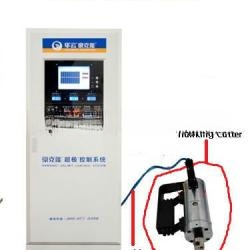
Most finishing equipment--Metal shaft finishing equipment
Price on request
Pricing is provided on request — use the quote form below.
- Port
- Qingdao
- Minimum Order Quantity
- 1 Set/Sets
- Supply Ability
- 1000 Set/Sets per Month
- Payment Terms
- L/C,T/T

Price on request
Pricing is provided on request — use the quote form below.
Something wrong with this listing? Report it
Ra0.2-0.8·20% better than before, depth is 0.1-0.2mm;·can completely keep the same accuracy as before, even better than before
| Condition | New | Place of Origin | Shandong China (Mainland) |
|---|---|---|---|
| Model Number | HKUSM30HSQ | Voltage | 220V±10% |
| Rated Power | 480 | Dimension(L*W*H) | 1000mm*400mm*800mm |
| Weight | 170kg | Certification | CE |
| Warranty | 1 year | After-sales Service Provided | Engineers available to service machinery overseas |
| Type of maching | arc surface | Value of roughness | Ra0.2-0.8 |
| Micro-hardness | raise 20% than before | Size accuracy | completely keep the same,even better |
| Vibration stress | preset compression stress and relief tentile stress | wear-resisting | raised a lot |
| corrosion resisting | raised a lot | micro defect | raised a lot |
| metal working life time | raised a lot | Details | Ra0.2-0.8 · 20% better than before, depth is 0.1-0.2mm; · can completely keep the same accuracy as before, even better than before |
| Packaging Detail | box |
|---|---|
| Delivery Detail | 30 days after advance payment |
Brief introduction of HawkingPTmetal work technology:
Processingafter before
Solutions of HawkingPTmetal work technology
HawkingPTHKUSM30G Series
Hawking VS Polishing P32 | ||
| Item | Hawking tech | Polishing |
| result | reach super mirror-finishing result of Ra≤0.2µm ; feeding between 50 and 80m/min | Ra1.6-0.8µm |
| efficience | line speed between 50 and 80m/min; feeding between 0.2 and 0.5 mm/r. efficient as the semi-superfinishing | inefficient |
| microhardness | improve 20% more than before | no change |
| fatigue | improve | no change |
| stress situation on metal surface | eliminate pulling stress on metal surface and preset perfect pressing stress | uncertainty |
| wear-resisting | improve | no change |
| corrosion resisting | improve | no change |
| quality on metal surface | even | uneven because of constant abrasing by grinding wheel |
| other materials consumption | no | using polishing whee,grinding material, abrasive belt etc. |
| procedure | not need moving the workpiece..Just clamp our equipment on the same lathe /machine tool | must move a workpiece to a polishing machine |
| operating envirenment | energy-efficient,enviroment protection,no sand & scrap iron | will leave some sand,scrap iron,dust , bad enviroment |
| suitability | best suitability,suitable for all kinds of surface shape | bad suitability, curved surface can not be processed |
| damage to a lathe/machine tool | no cutting and no damage to a lathe | sands left over can damage the part of rail road on the lathe |
| operating room | need a little space to set our equipment | special operating room, spcial space |
| possibility of danger | no | grinding wheel might damage an operator |
P33
Hawking VS Cylindrical grinding | ||
| Item | Hawking tech | Cylindrical grinding |
| result | reach super mirror-finishing result of Ra≤0.2µm ; feeding between 50 and 80m/min | Ra1.6-0.8µm |
| efficience | line speed between 50 and 80m/min; feeding between 0.2 and 0.5 mm/r. efficient as the semi-superfinishing | inefficient |
| microhardness | improve 20% more than before | no change |
| fatigue | improve | no change |
| stress situation on metal surface | eliminate pulling stress on metal surface and preset perfect pressing stress | uncertainty |
| wear-resisting | improve | no change |
| corrosion resisting | improve | no change |
| suitability for meta materials | can process a hard,soft and sticking metal materials | can not process a soft and sticking metal materials |
| environment protection | very good,nothing left | leave sand and junk cooling liquid |
| energy consumption | very little,the power is less than 1kw | very big, the power must be more than many kw |
| procedure | not need moving the workpiece..Just clamp our equipment on the same lathe /machine tool | must move a workpiece to a polishing machine |
| other materials consumption | no | using grinding wheel and cooling liquid |
P34
Steps of Hawking VS Normal grinding | ||
| Step | Hawking tech | Normal grinding |
| 1 | use a suitable cutter imported from Switzerland to get a basic size and geometrical tolerance meeting the requirement of drawing. Roughness is Ra2.1µm. | use a Kenner KT315 cutter to get a basic size and geometrical tolerance meeting the requirement of drawing by finish maching. Roughness is between Ra3.2 and 6.3µm. |
| 2 | use a Hawking cutter clamped on the lathe to process (line speed of processing is 39 m/min, feeding is 0.3mm/r) | it will take72 hoursto manually grind a work piece by using a millstone with No.150 diamond grain. In order to completely eliminate the screwing wave during grinding. |
| 3 | done intwo daysfrom size precision to mirror finishing level.Value of Ra between 0.07 and 0.1µm | it will take24 hoursto semi-grind a work piece by using a millstone with No.180 diamond grain. |
| 4 | better than what the design requires | it will take16 hoursto grind a work piece by using a millstone with No.240 diamond grain. |
| 5 | it will take3 hoursto polish a work piece by using W7 polishing paste and kerosene on lathe when the top spinning speed is 40r/min and line speed about 300m/min . | |
| 6 | roughness between Ra0.16 and 0.2µm,meet the requirement | |
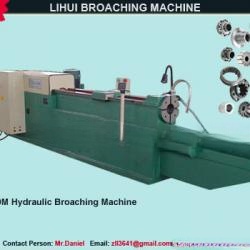
30T gray cast iron frame hydraulic broaching machining machinery
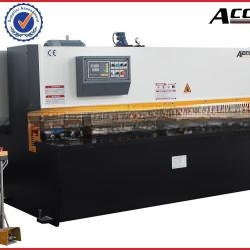
Hydraulic Plate Shearing Machine,Sheet Metal Shearing Machine for Accurl
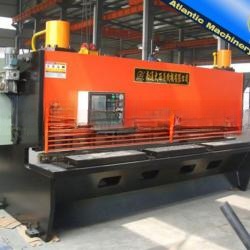
metal shear machine QC11Y-20*2500
Electric hydraulic portable bar rebar steel cutter 4mm - 25mm
slitting head JB1400mm slitting machine
ZQ11 Hydraulic Sheet Metal Shearing Machine