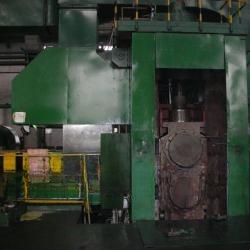
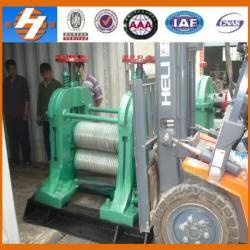
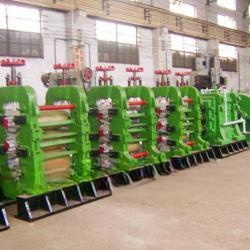
irreversible aluminum foil cold rolling mill
A, process outline:
1.1. Rolling material:
Material: tin and alloys
Slab: ~ 25 mm thick 500 mm ~ 700 mm wide length: 200 ~ 500 mm
1.2. Rolling finished product:
Material: tin and alloys
Plate: finished thickness: 8 ~ 10 mm width: 500 ~ 700 mm length: more than 1500 mm
1.3. Equipment design and manufacturing range:
300 x 800 two roll hot rolling mill 1 set Include:
1) press 1 set of devices
2) frame 1 set of assembly
3) roll assembly 1 set
4) main transmission device 1 set (the Lord deceleration machine, main motor, one word gear box, connecting shaft, coupling)
5) 1 set of control system
6) before and after each one set of the roller
B, equipment supporting process and technical parameters:
2.1 the mill work form: reversible
2.2 technological process:
A plank: thick 25 mm , wide 500 ~ 700 mm billet reheating furnace, the heat the process need to temperature, the stove with tongs to have laid right of rolling mill roll gap for the first time, A rolling passes under the pressure of 30%, rolling mill, the second set after reverse way time roll gap, material is passed back, so passive roller about 3 ~ 7 way, average of reduction control in 25 ~ 30% into talents. (a process is complete)
this machine is mainly used to roll average routine steels,ideformed steel,copper,aluminum product.
aluminum steel,steel window and other steels.that wre used and srap.
use explanation:
the aluminum beillt seminfinished product continuous casting tanden rolling craft was introduced from the overseas in the 80's .that advanced technique of production .
it's basic flow was:aluminum ingot--smelting furnace--settlement stove--deaeration--filtration--casts month--grips machine--middle unit--coiler
| Type | | 1 | 550 × 650mm | | 2 | 600 × 1000mm | | 3 | 650 × 1200mm | | 4 | 680 × 1450mm | | 5 | 690 × 1650mm | | 6 | 850 × 1750mm | | 7 | 960 × 1850mm | | 8 | 1020 × 2000mm |
|